Dibond, Alupanel, Hylite: fast cutting and folding grooves of perfectly constant depth, on both the VSR and the LT.
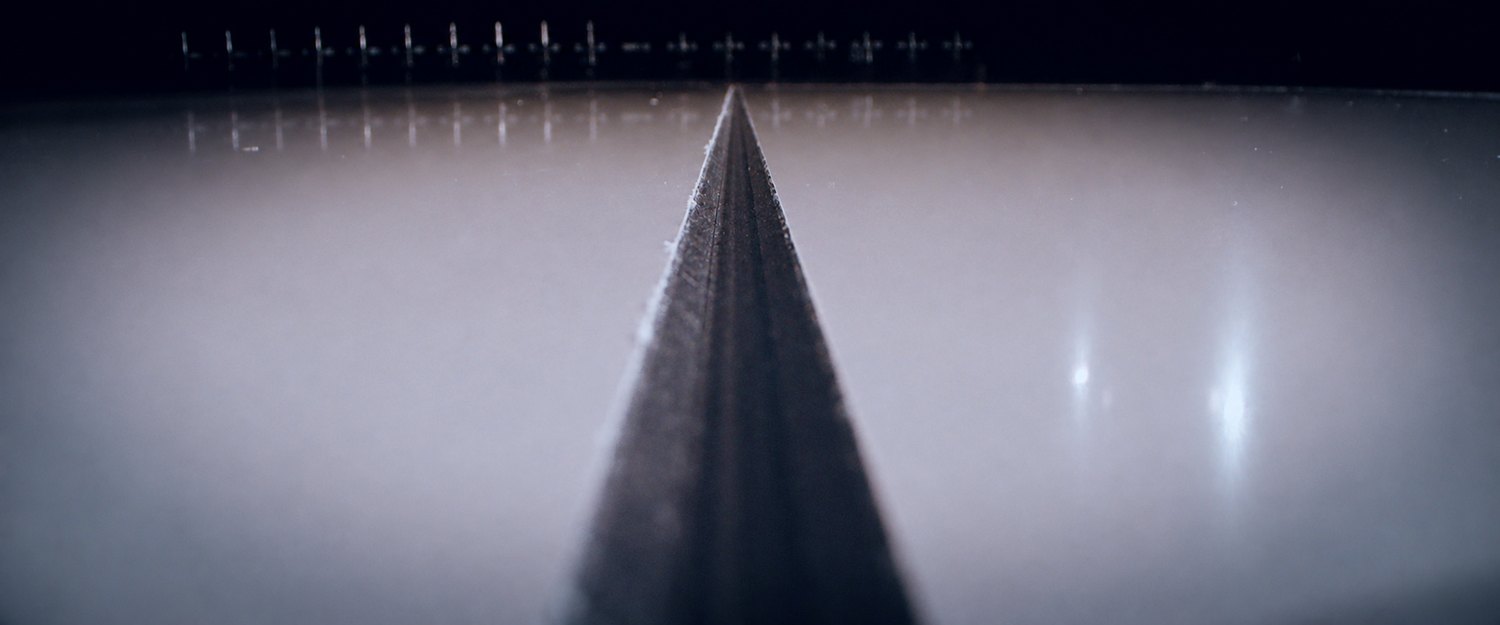
To fold an aluminium composite panel – trays, posts, boxes – you need a groove of strictly constant depth. For a 90° fold, a 95° V-groove bit with a flat of about 1 mm is typically used, leaving only 0.4 to 0.5 mm of material at the bottom of the groove.
With a quality cutter, grooving reaches 15,000 mm/min without difficulty. Note: many off-the-shelf cutters only allow 4,000 to 5,000 mm/min.
The dimension that determines a perfect fold is the material remaining between the table and the tip of the cutter. It is therefore not necessary to probe the aluminium composite; on the other hand, the table geometry must be followed perfectly throughout machining.
This is what the VSR and the LT do: they continuously compensate the table flatness and produce regular folding grooves over their entire length.
Cutting is done with a straight carbide end mill with a right-hand helix, ideally coated. For large shapes or large panels, a larger-diameter cutter saves time.
| Operation | Thickness | Tool | Feed rate | Spindle |
|---|---|---|---|---|
| Cutting small parts | 3 mm | 4 mm straight end mill | 2,600 mm/min | 24,000 rpm |
| Cutting large shapes | 3 mm | 6 to 8 mm straight end mill | 8,000 to 10,000 mm/min | — |
| Grooving for a 90° fold | 3 mm | 95° V-groove bit, ≈ 1 mm flat | Up to 15,000 mm/min | — |
Indicative values: they depend on the material, the expected result, and the quality and wear of the cutter.
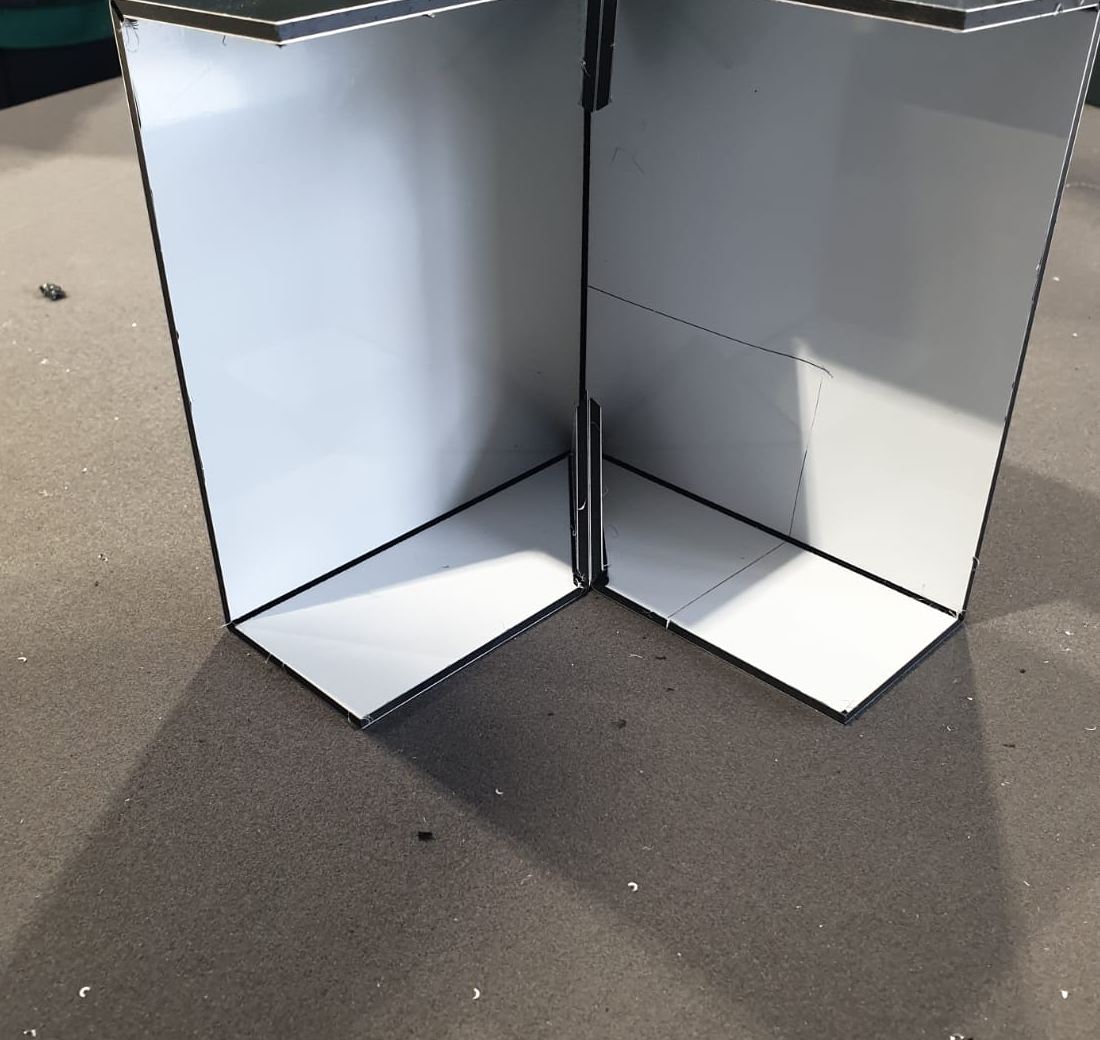
Hylite: thanks to the tracking of the table geometry, VERSO machines can produce front and back hinges in this aluminium composite.
Typically a 95° V-groove bit with a flat of about 1 mm. With a quality cutter, grooving can reach 15,000 mm/min on VERSO machines; many off-the-shelf cutters only allow 4,000 to 5,000 mm/min.
To make Dibond trays, the machine must leave only 0.4 to 0.5 mm of material at the bottom of the groove. This dimension, measured between the table and the tip of the cutter, determines the quality of the fold.
No. However, the table geometry must be followed perfectly throughout machining. This is the case on the VERSO VSR and LT, which produce regular folding grooves over their entire length.
As an indication: for small parts, 4 mm end mill, 2,600 mm/min, spindle at 24,000 rpm. For large shapes, a 6 to 8 mm end mill allows 8,000 to 10,000 mm/min.
Yes. Thanks to the tracking of the table geometry, VERSO machines can produce front and back hinges in Hylite.
Transparent edges without polishing, engraving, tapping, Bloc-LED.
No coolant, coated end mills, tapping up to M10.
Species, panels, compression bit, okoumé, rubberwood.
Forex at 60 m/min with a knife, solid PVC without melting.
POM, nylon, PE, PTFE, fibreglass, sandwich panels.
Vinyl, cardboard, foams, leather, rubber, Stadur, Akylux…
Overview and summary table: all machinable materials.
Full machine specifications: VSR technical specifications · LT technical specifications.
Contact us for a demonstration or a personalised quote.
Contact us